

 English
 中文简体
 русский
 Français
 Español
 Deutsch
YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine for Advanced Composite Fabrics
2026-11-06
Content
- 1 Overview of the YRS3-M-F-II Platform
- 2 Core Technical Characteristics
- 3 How the Machine Produces Directional Chopped-Fiber Fabrics
- 4 Advantages of Directional Biaxial Construction
- 5 Advantages Compared with Alternative Equipment
- 6 Fabric Construction and Product Options
- 7 Applications in Wind Power and Composite Manufacturing
- 8 Manufacturing Strengths of Changzhou Yuanyang Electromechanical Technology Co., Ltd.
- 9 Configuration Process for a New Project
- 10 Installation, Commissioning and Training
- 11 Maintenance and Long-Term Serviceability
- 12 Quality Control in Fabric Production
- 13 Operational Benefits for Composite Textile Producers
- 14 Frequently Asked Questions
- 14.1 What type of machine is the YRS3-M-F-II?
- 14.2 Which fibers can be processed?
- 14.3 Can the 0°/90° weight ratio be customized?
- 14.4 What is the available chopped-layer weight?
- 14.5 Can a nonwoven layer be used?
- 14.6 What is the typical finished fabric weight?
- 14.7 What is the machine’s working width?
- 14.8 What output can be expected?
- 14.9 Is the machine suitable for wind-power fabrics?
- 14.10 How does the HS version differ from the HX version?
- 14.11 Does the supplier provide installation and training?
- 14.12 Can the machine be customized?
- 15 Conclusion
- 16 References
- 17 Product: YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine(HS)
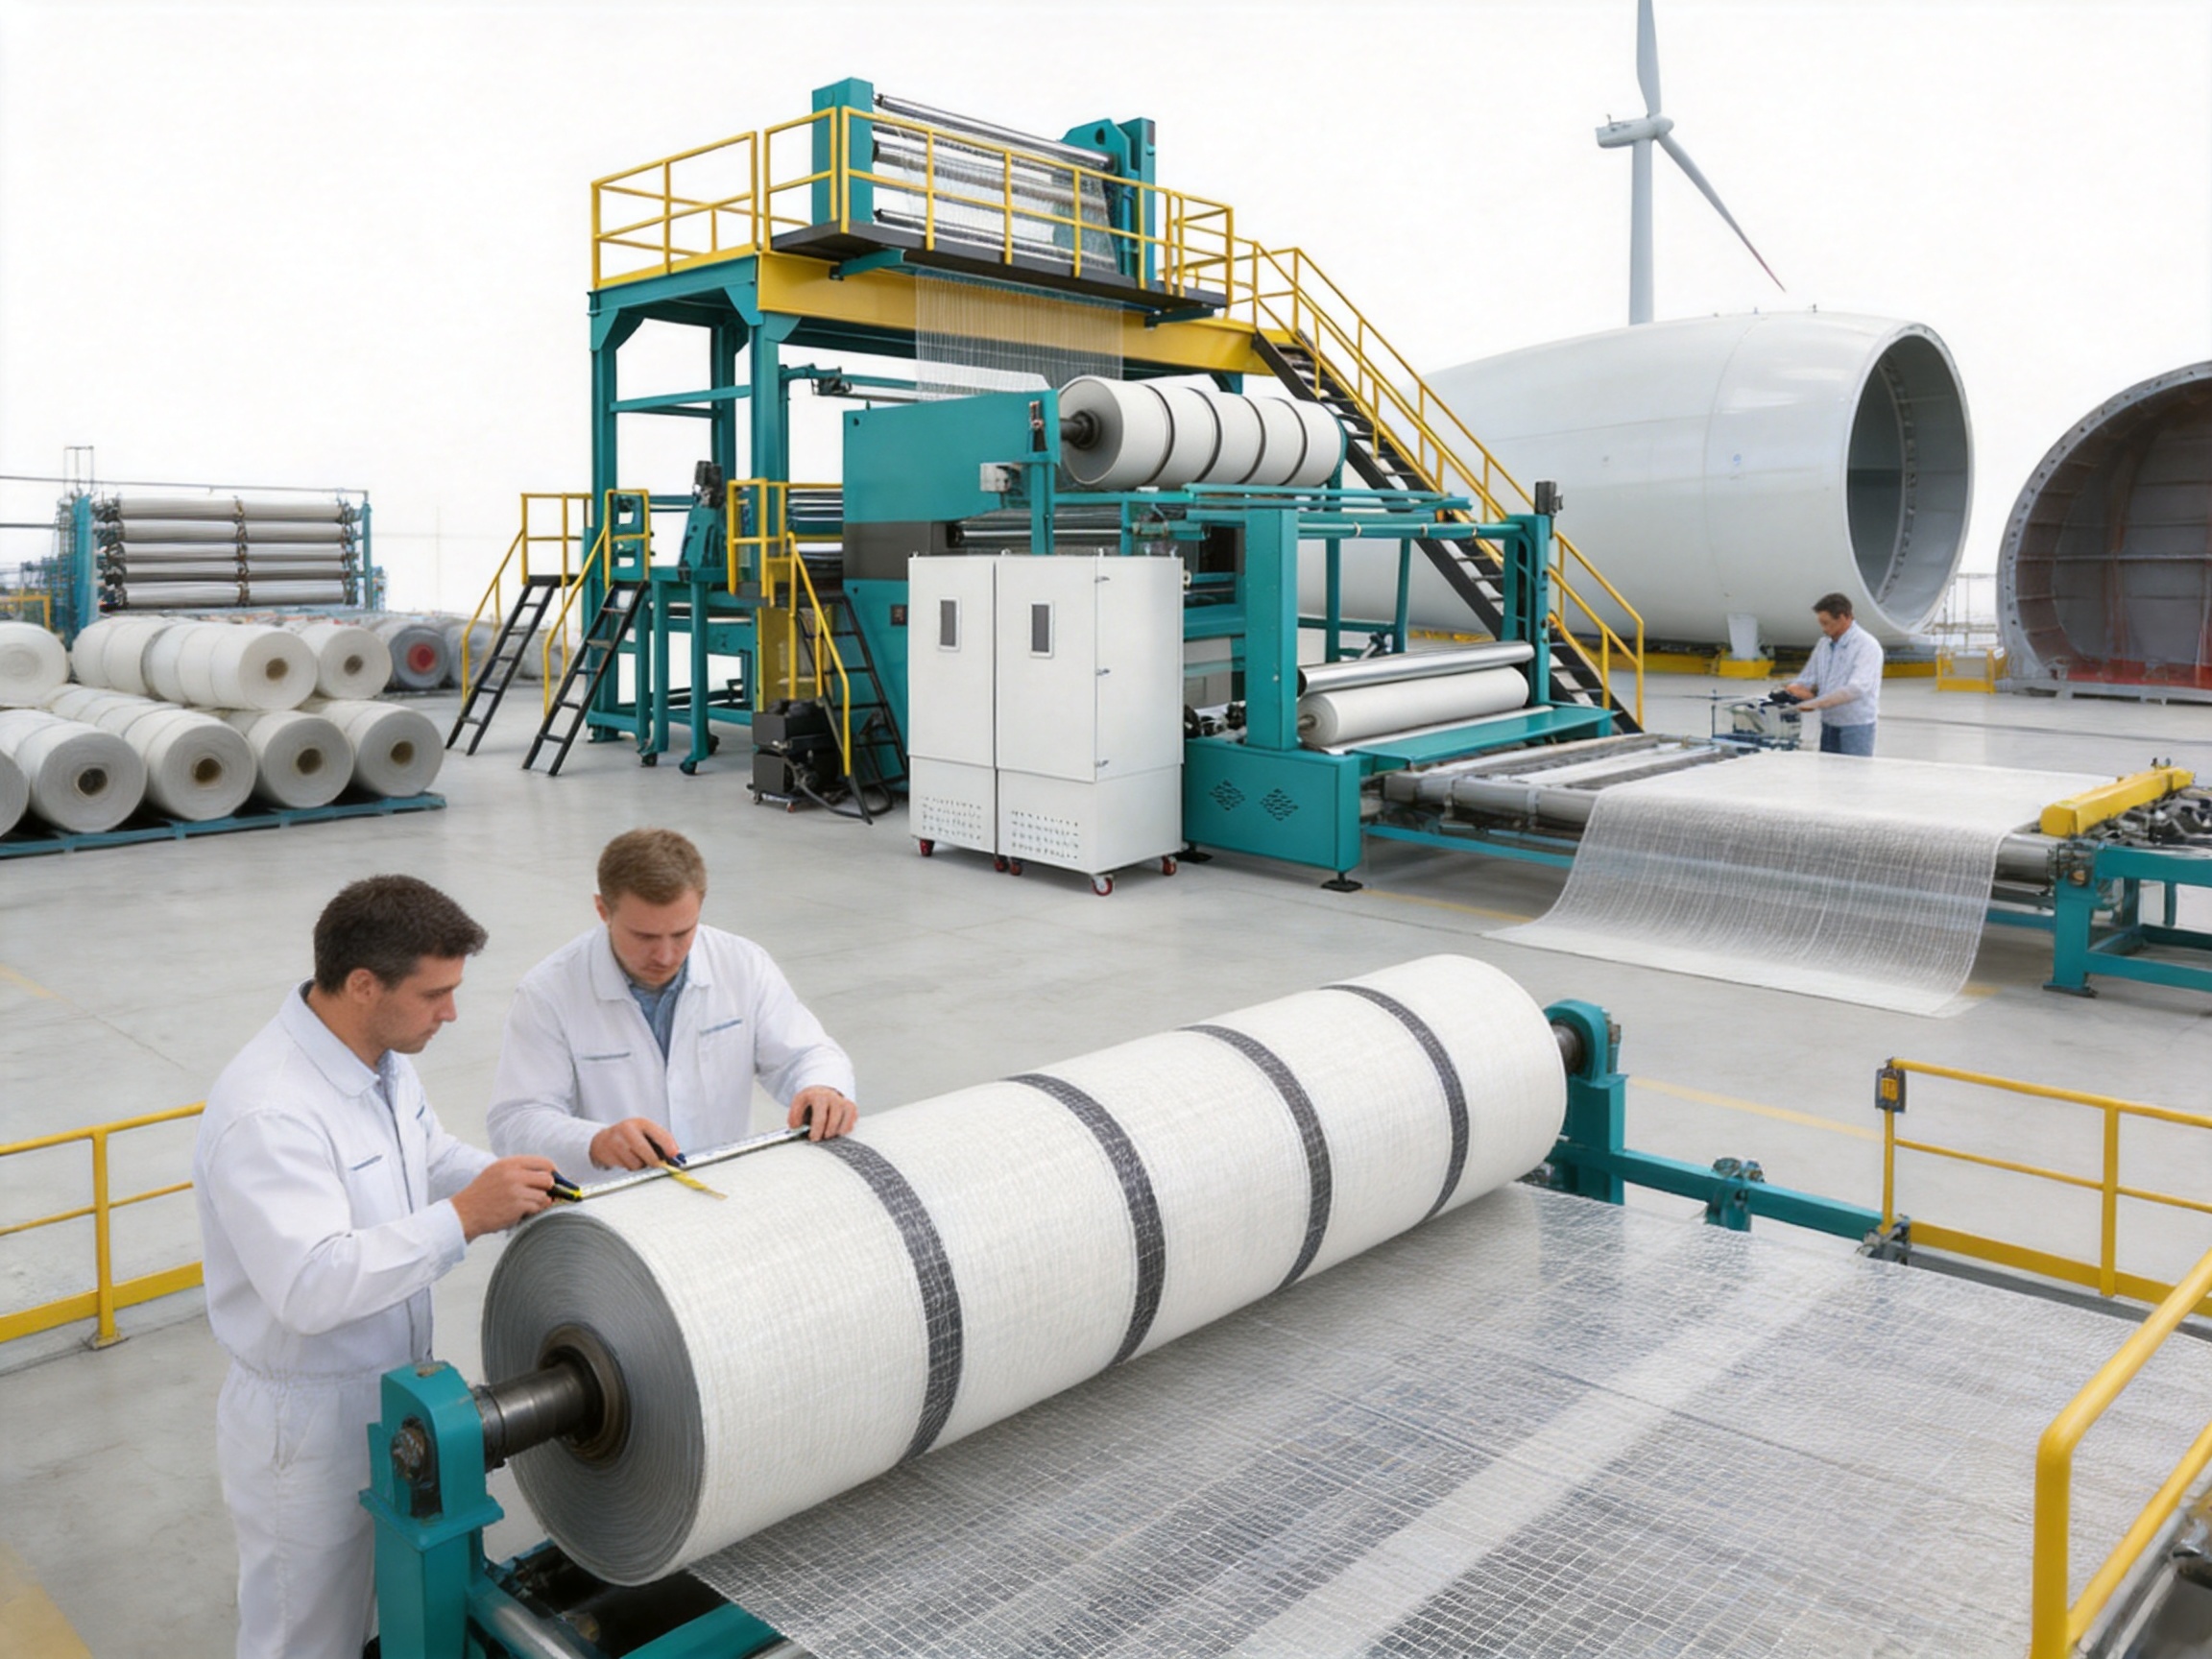
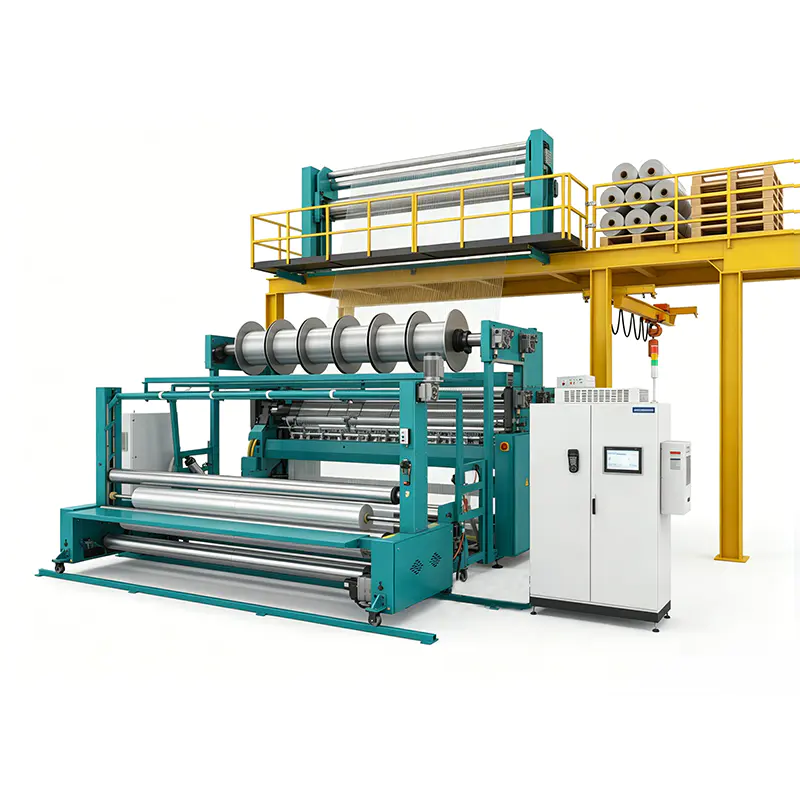
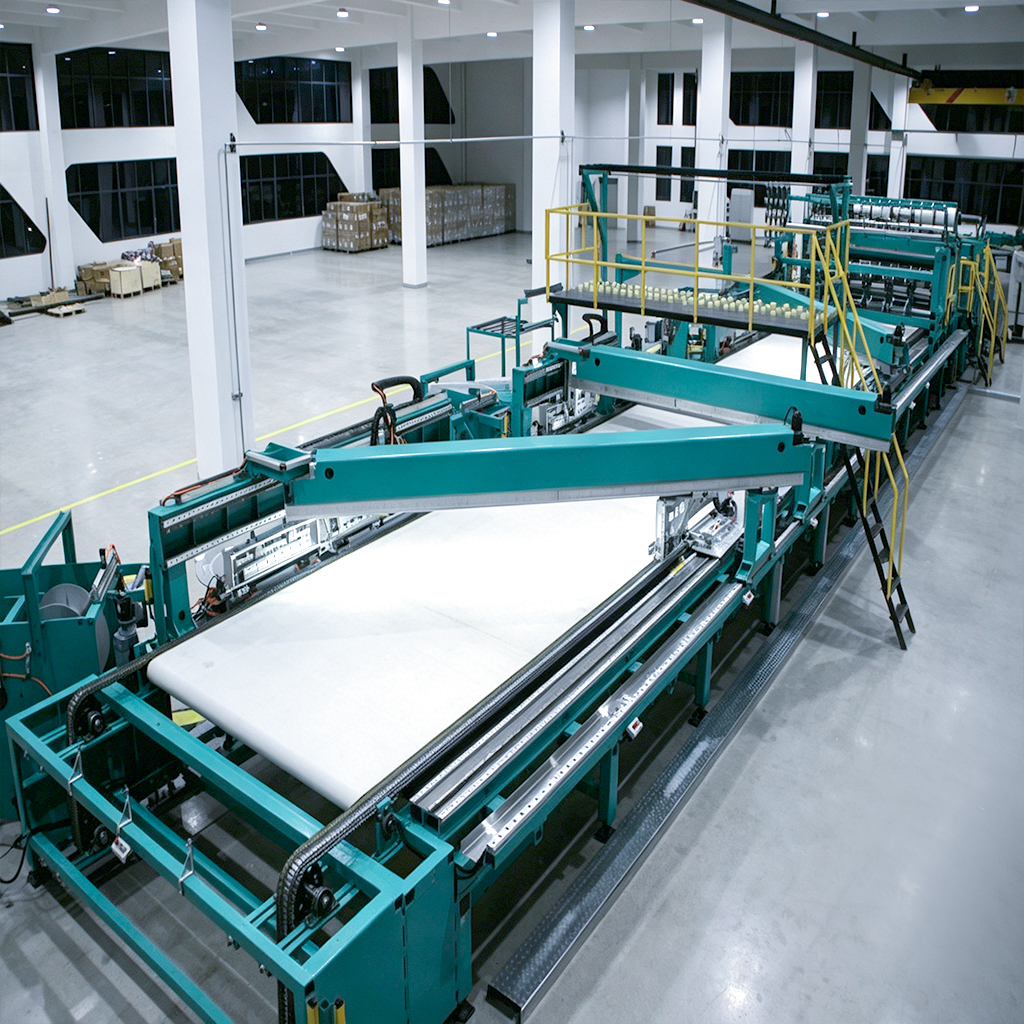
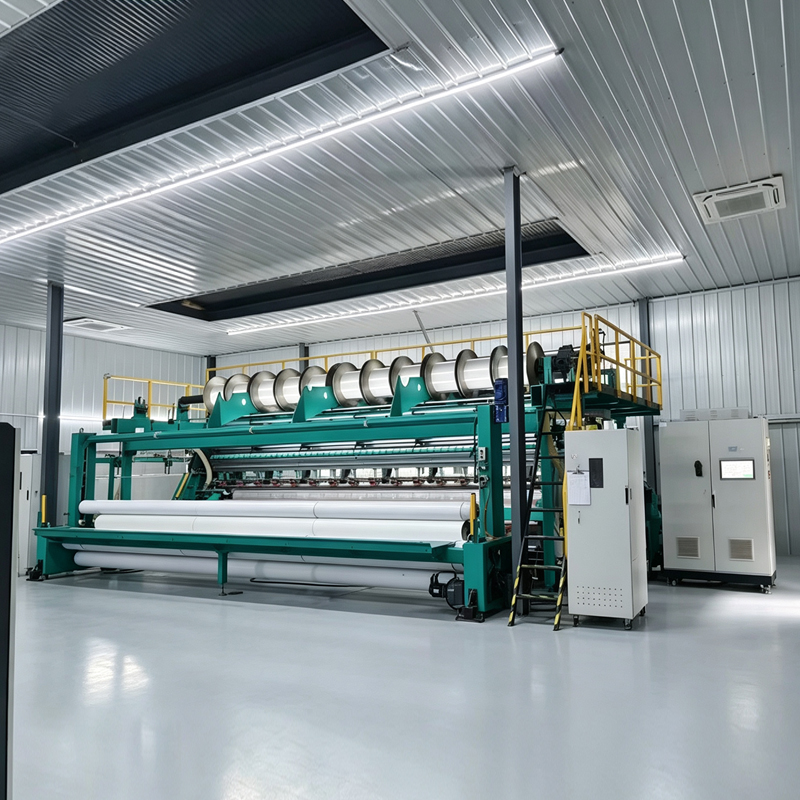
The YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine is a specialized production platform for manufacturers of fiberglass reinforcement fabrics, composite textiles and directional chopped-fiber mats. By combining 0°/90° weft insertion, warp knitting and an integrated chopping unit, the machine produces fabrics with an organized reinforcement structure, controlled directional balance and efficient forming performance.
Unlike conventional randomly oriented chopped strand mat equipment, this machine creates a more deliberate textile architecture. The principal yarn systems are placed in defined machine and cross-machine directions, while an optional chopped layer or nonwoven substrate can be introduced beneath the yarns. This construction gives composite manufacturers greater control over areal weight, directional reinforcement, resin flow and laminate design.
The machine is intended for demanding applications including wind-power components, nacelle covers, composite shells, industrial reinforcement products and other structures requiring stable, high-volume fiberglass textile production. Its working width, speed range and configurable material system allow it to be adapted to different fabric constructions and production targets.
Overview of the YRS3-M-F-II Platform
The YRS3-M-F-II is a biaxial warp knitting machine configured with a chopping unit. It is designed to manufacture full-width weft-inserted fabrics in which the 0° and 90° reinforcement directions can be adjusted according to the required product specification.
Warp yarns generally follow the machine direction, while the weft yarns are inserted across the working width. The knitting system binds these yarns into a stable textile structure. When required, the chopping unit places chopped fiber into the fabric system, allowing the machine to produce a combined reinforcement construction rather than a simple two-directional stitched fabric.
The resulting material can be engineered as a full-width weft-inserted chopped mat, a composite reinforcement fabric or a hybrid structure incorporating a nonwoven layer. The final fabric weight typically ranges from 300 to 2000 g/m², while the optional chopped layer can be configured from 50 to 500 g/m².
Because the machine is configured around the target fabric rather than a single fixed textile recipe, users can define the 0°/90° weight ratio, chopped layer requirement, nonwoven feed requirement, yarn type and desired production speed. This makes the platform suitable for both standard reinforcement products and application-specific composite fabrics.
Core Technical Characteristics
| Item | Specification | Production Significance |
|---|---|---|
| Machine type | Raschel chopped fiber biaxial warp knitting machine | Combines warp knitting, biaxial weft insertion and chopped-fiber integration |
| Applicable fibers | Glass fiber and polyester | Supports common reinforcement and binding yarn systems |
| Machine speed | 50–1000 r/min | Allows the operating window to be matched to fabric construction |
| Working width | 103 inches, 0°/90° | Provides a broad production format for industrial composite fabrics |
| Directional lay | 0°/90° | Directional weight ratio can be customized |
| Optional chopped layer | 50–500 g/m² | Permits integrated chopped-fiber reinforcement beneath the yarns |
| Typical greige fabric weight | 300–2000 g/m² | Accommodates light, medium and heavy reinforcement constructions |
| Reference daily output | Up to 3000 kg per day | Actual output depends on fabric design and process conditions |
The stated production values are reference figures. Actual performance depends on fiber type, yarn tex, package format, fabric weight, directional ratio, stitch pattern, chopped-layer weight, machine settings, operator skill and downstream handling. During project configuration, these factors are reviewed together so that the machine is matched to a realistic production target.
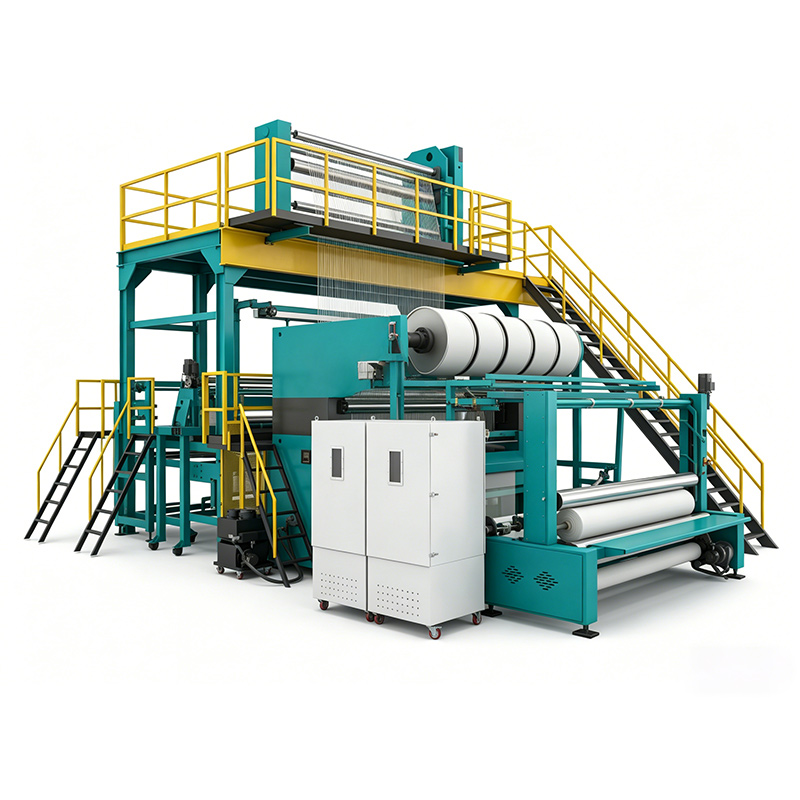
YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine(HS)
How the Machine Produces Directional Chopped-Fiber Fabrics
The production process begins with the preparation of the yarn and fiber supply system. Glass fiber or polyester yarn packages are arranged according to the desired fabric construction. Yarn tension, package geometry and creel layout are important because reinforcement yarns must remain stable as they enter the knitting and insertion zones.
Warp yarns are guided through the machine in the longitudinal direction. These yarns contribute to the machine-direction reinforcement and also participate in the formation of the knitted binding structure. Their tension must be controlled carefully to prevent irregular stitch formation, edge instability or variation in fabric density.
The 90° weft yarns are inserted across the working width. The quantity and density of these yarns determine the cross-machine reinforcement level. By adjusting the relative contribution of the 0° and 90° yarn systems, the producer can manufacture a fabric with a balanced structure or a deliberately unbalanced structure designed for a particular laminate or component.
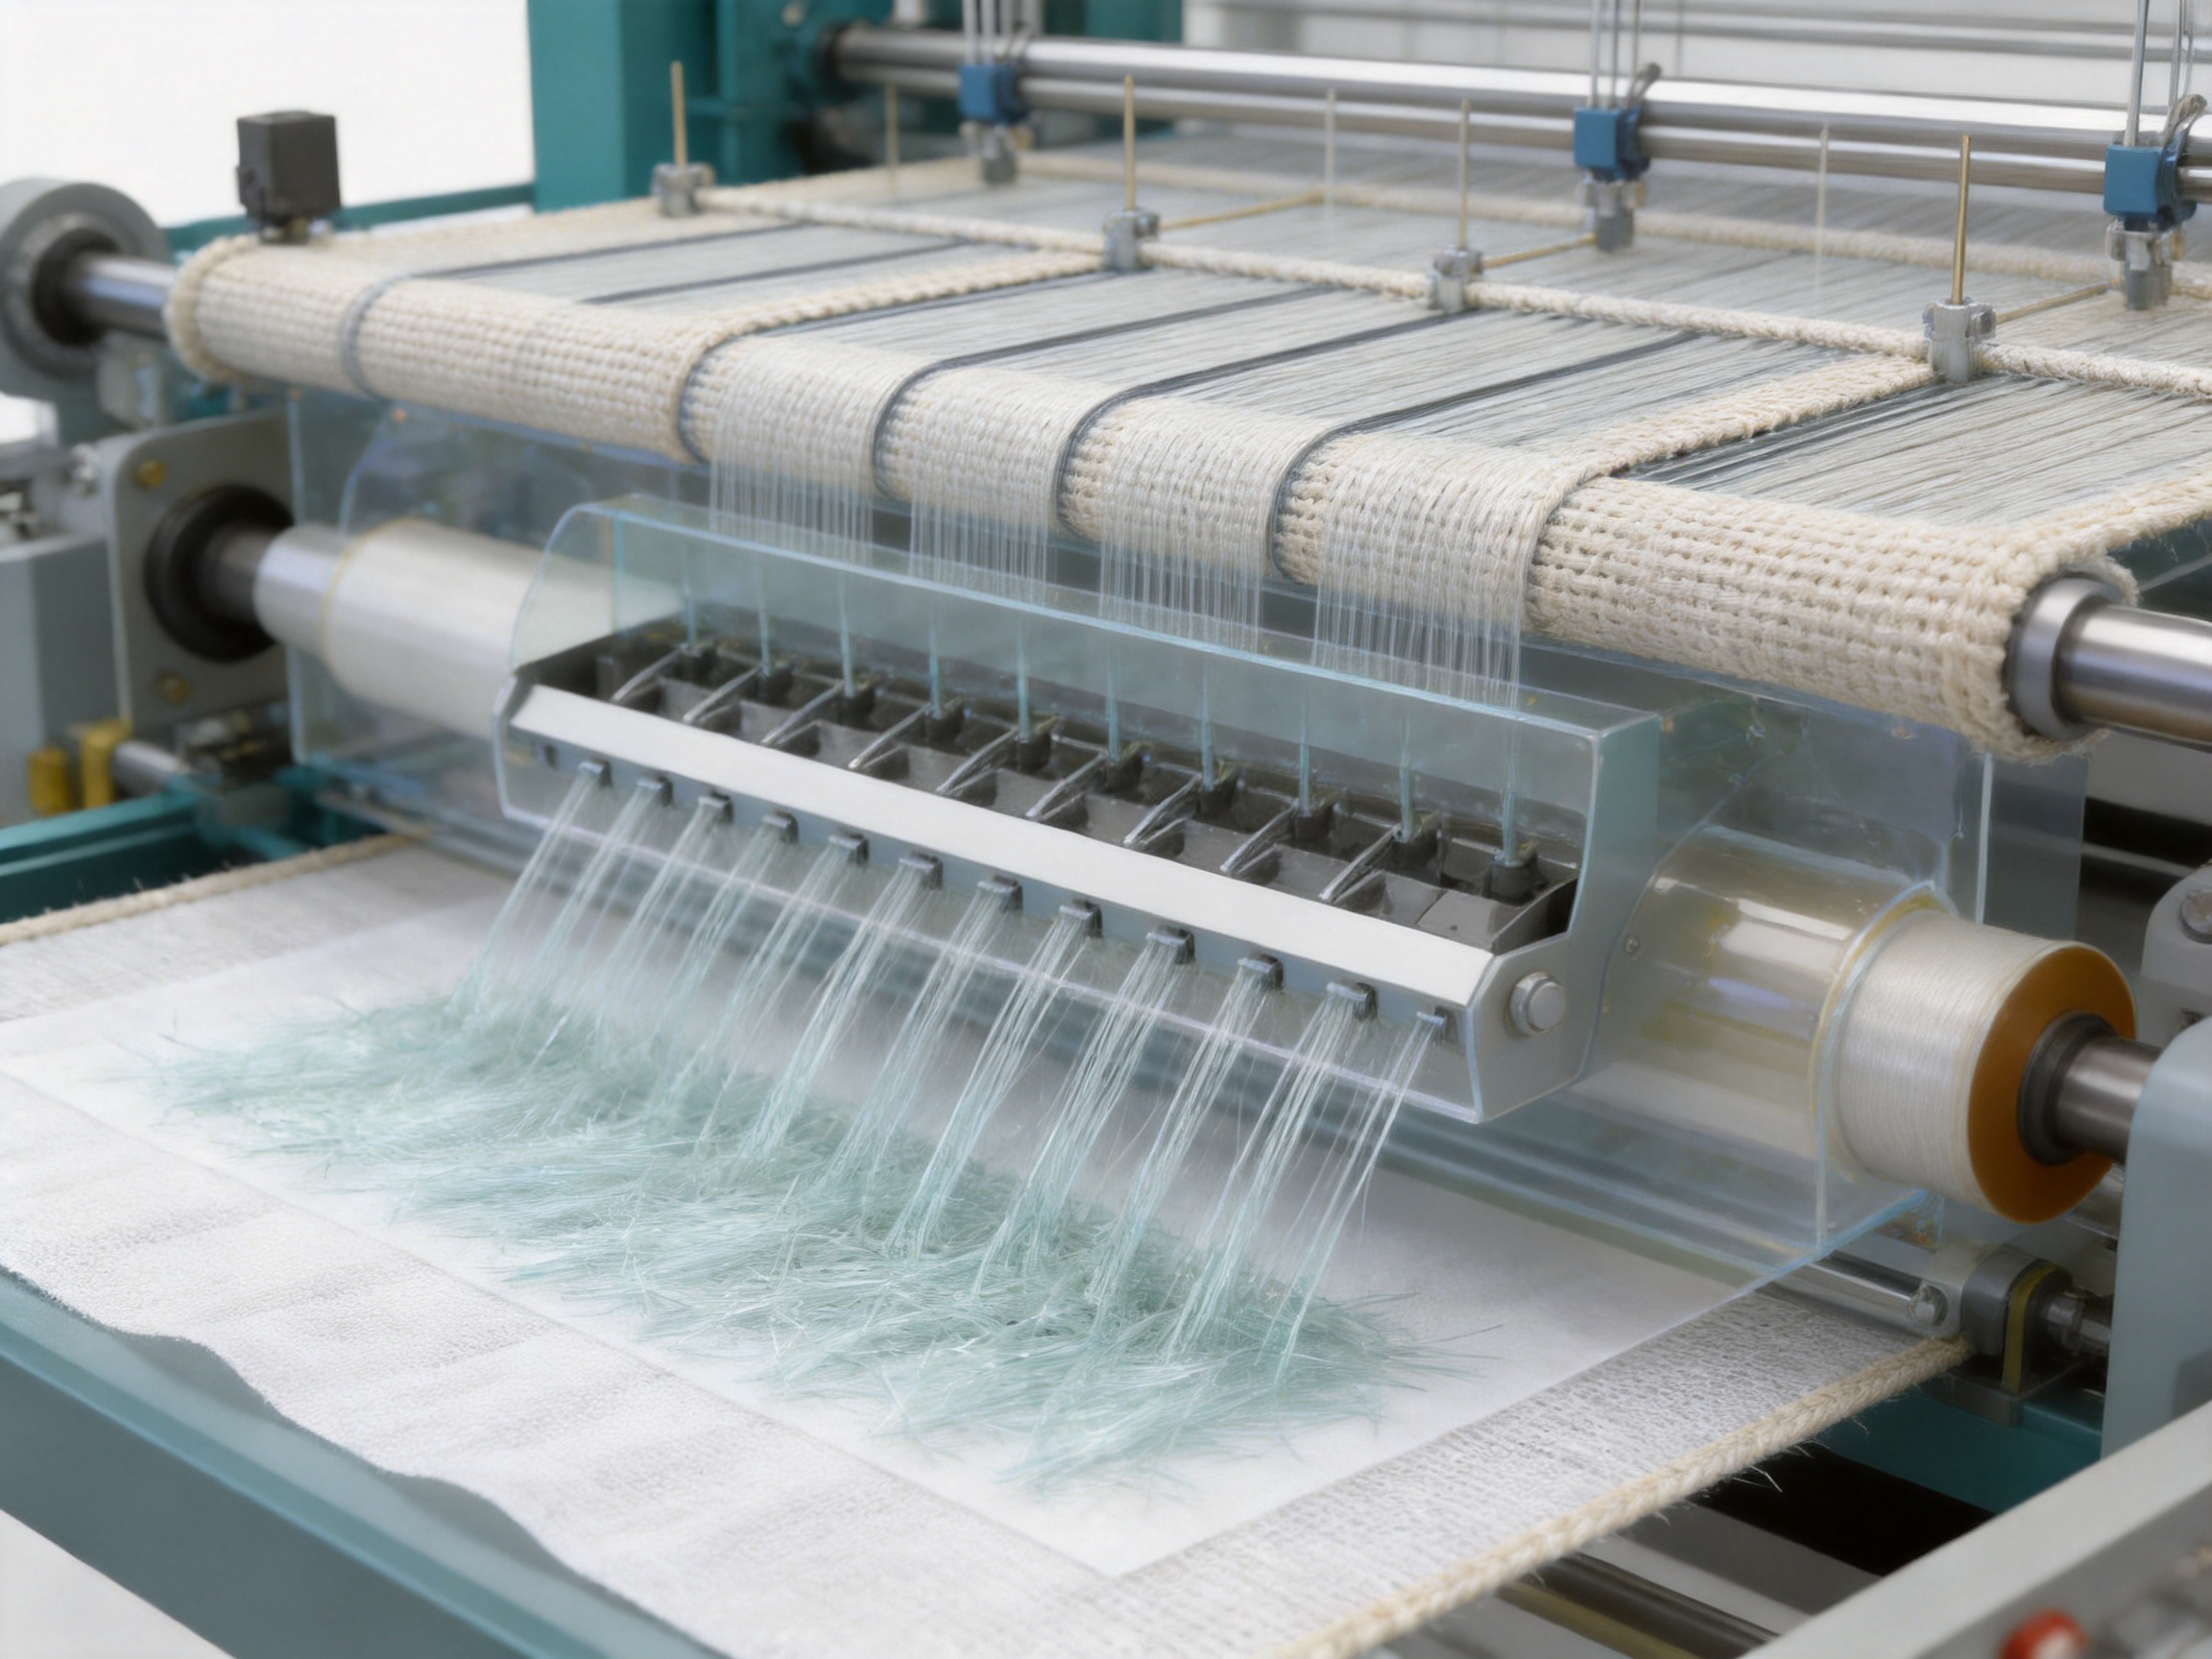
The chopping unit introduces chopped fiber when the product specification requires an additional random or semi-distributed fiber layer. This layer can be positioned beneath the principal yarn systems, where it contributes bulk, surface coverage, resin distribution and additional reinforcement. The chopped material is then integrated into the knitted fabric structure.
A nonwoven substrate can also be used in place of, or in combination with, the chopped layer where the final product requires a defined carrier, surface veil or resin-flow medium. The ability to introduce this material on the same platform reduces the need for separate handling operations and can simplify the overall production line.
After the yarns, chopped fiber and optional substrate have been combined, the knitting elements stabilize the structure. The machine therefore produces a fabric that is more organized than a conventional random mat while retaining the useful forming characteristics of a chopped-fiber textile.
Advantages of Directional Biaxial Construction
The principal advantage of the YRS3-M-F-II is its ability to combine directional reinforcement with an optional chopped-fiber layer. Conventional chopped strand mats generally provide broadly distributed reinforcement but offer limited control over the proportion of material aligned in specific directions. A basic biaxial fabric provides directional control but may not offer the same surface coverage, bulk or forming behavior as a chopped mat.
This machine bridges those requirements. It allows the producer to define the main reinforcement directions while adding a chopped or nonwoven component according to the application. The result is a more versatile textile architecture for composite processing.
A controlled 0°/90° ratio is valuable when the final component is exposed to different loads along its length and width. Wind-power structures, covers and composite panels often require specific stiffness or strength behavior in more than one direction. By adjusting the yarn balance, the fabric can be matched more closely to the intended laminate design.
The ordered weft placement also supports predictable handling. Parallel yarns are easier to identify and control during cutting, stacking and lamination. This can be especially useful when a fabric is supplied to automated or semi-automated composite manufacturing operations.
The integrated chopped layer adds another level of flexibility. It can improve local coverage between the directional yarns, contribute to surface continuity and support resin distribution. In a multilayer laminate, this type of material can be selected to work alongside directional plies and other core or surface materials.
Advantages Compared with Alternative Equipment
Compared with Conventional Chopped Strand Mat Lines
Conventional chopped strand mat equipment is effective for producing randomly oriented fiber mats, but it generally does not provide the same degree of 0°/90° directional control. The YRS3-M-F-II gives manufacturers the option to retain a chopped layer while establishing a defined biaxial reinforcement framework.
This can reduce the need to combine separate rolls of random mat and biaxial fabric during laminate preparation. Depending on the product design, a combined fabric may simplify material selection, reduce handling steps and improve consistency between production batches.
Compared with Basic Biaxial Warp Knitting Machines
A standard biaxial warp knitting machine can produce directional reinforcement fabrics, but it may not include the chopping unit or the associated feed arrangement. The YRS3-M-F-II is designed for manufacturers that need to integrate chopped fiber or a nonwoven layer during the same production sequence.
This integrated approach is particularly useful when the final textile must combine directional reinforcement, surface coverage and controlled areal weight. It also enables a producer to serve more product categories without installing a completely separate chopped-mat line.
Compared with Separate Fabric Assembly Operations
Some composite manufacturers assemble several textile layers after individual materials have been produced. While this method remains suitable for certain products, it can introduce additional unwinding, alignment, storage and inspection requirements. A configured YRS3-M-F-II line can combine important components during production, reducing the number of independent handling stages.
Fewer handling stages can help reduce the risk of misalignment, contamination, incorrect layer selection or variation in roll structure. The exact benefit depends on the final product, but integrated production generally offers a stronger basis for repeatable material construction.
Compared with Fixed-Configuration Machinery
Many machines are optimized for one fabric type, one weight range or one fixed reinforcement ratio. The YRS3-M-F-II is configured around the customer’s material requirements. Its adjustable directional ratio, optional chopped layer and optional nonwoven feed provide a wider operating scope than a machine designed for only one construction.
This flexibility is valuable for textile producers that serve several composite markets. The same basic platform can be adapted for different areal weights, fiber package formats and reinforcement recipes, subject to the confirmed mechanical and process configuration.
Fabric Construction and Product Options
The YRS3-M-F-II can manufacture full-width weft-inserted chopped mats and composite fabrics. The precise construction is agreed during technical review, taking into account the required laminate performance, processing method, roll dimensions and downstream equipment.
The 0°/90° weight ratio is one of the most important configuration variables. A balanced ratio may be appropriate for applications that require similar reinforcement in both principal directions. An unbalanced ratio may be selected where the finished component experiences a higher load in one direction.
The optional chopped layer is generally specified between 50 and 500 g/m². A lower chopped-layer weight may be selected when the directional yarn system remains the principal reinforcement and only additional coverage or surface continuity is required. A higher value may be suitable when the product requires more substantial chopped-fiber content.
A suitable nonwoven fabric can also be introduced beneath the yarns. The nonwoven component may act as a carrier, surface layer or process-support material. The exact material must be reviewed against the fiber type, resin system, bonding requirements and temperature conditions of the intended application.
Greige fabric weight typically falls within the 300–2000 g/m² range. This broad range allows the equipment to support relatively light composite textiles as well as heavy reinforcement fabrics for industrial structures. The achievable result depends on the combination of yarn density, stitch formation, chopped-layer content and machine operating conditions.
Applications in Wind Power and Composite Manufacturing
Wind-power components require reinforcement textiles that can be supplied in large formats, processed consistently and adapted to complex load conditions. The YRS3-M-F-II is positioned for wind-power fabrics and nacelle-cover applications because it can produce broad, directional reinforcement structures with optional chopped or nonwoven layers.
For nacelle covers and related composite housings, the fabric may need to combine handling stability, surface coverage and controlled reinforcement. The 0°/90° structure supports load distribution, while the chopped layer can help reduce open areas between principal yarns and contribute to a more continuous textile surface.
The machine can also serve composite panel manufacturers, molded-cover producers, industrial equipment suppliers and reinforcement textile converters. Its ability to process glass fiber and polyester makes it appropriate for a wide range of glass-reinforced polymer production systems.
Other potential uses include structural shells, transportation components, construction panels, marine composite products and industrial laminates. Each application requires separate confirmation of resin compatibility, target fabric weight, roll format and mechanical performance.
Manufacturing Strengths of Changzhou Yuanyang Electromechanical Technology Co., Ltd.
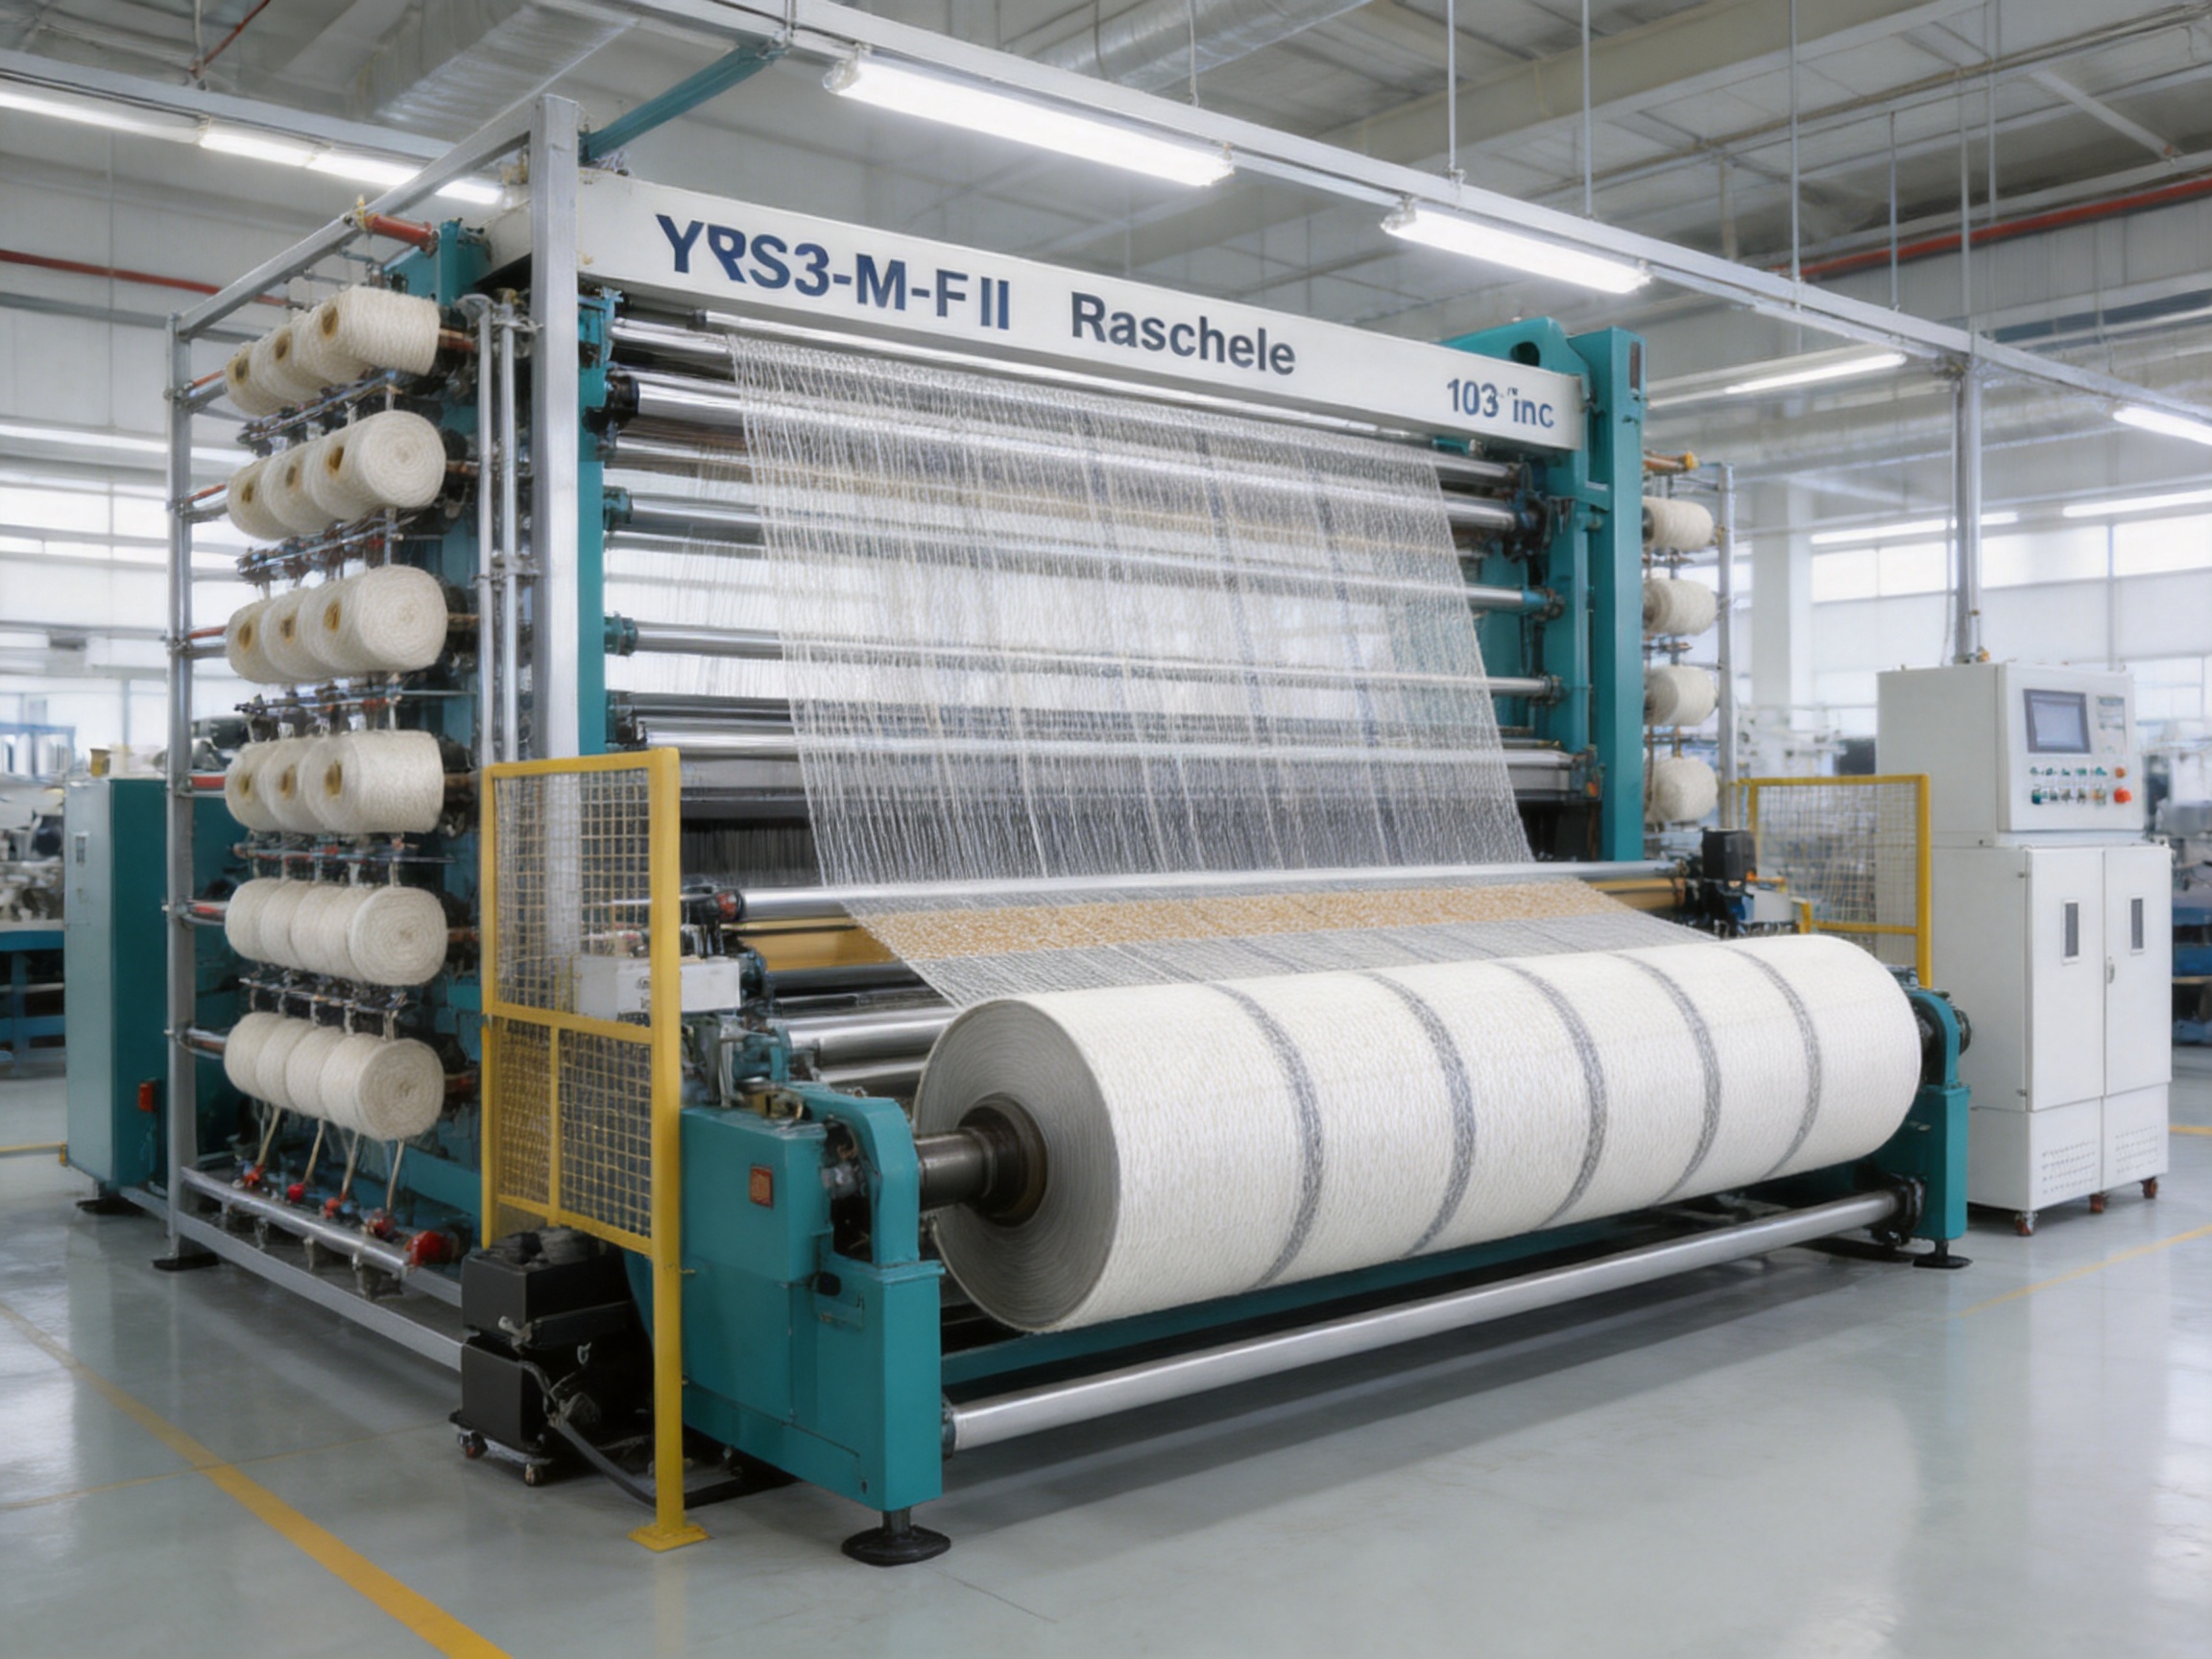
Changzhou Yuanyang Electromechanical Technology Co., Ltd. develops and manufactures warp knitting equipment and related specialty textile machinery. Its product range includes stitch-bonding machines, biaxial warp knitting machines, multiaxial warp knitting machines, carbon-fiber multiaxial warp knitting machines, powder scattering machines and web-laying machines.
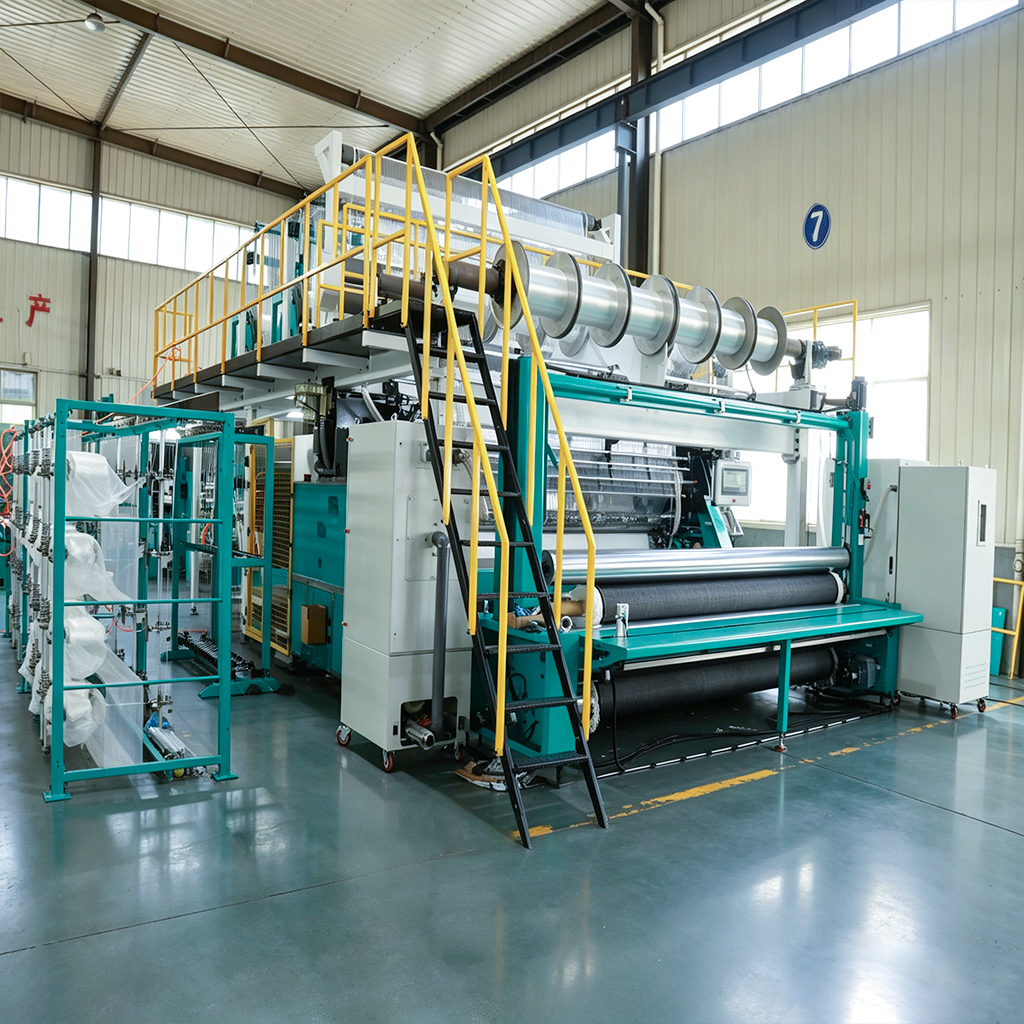
The company’s manufacturing capability is supported by a production base of more than 12,000 square meters, standardized workshops, an intelligent warehouse and dedicated inspection areas. These facilities allow the production process to be organized across component procurement, machining, assembly, functional testing and final debugging.
Rather than treating the machine as a collection of unrelated components, the manufacturing process coordinates the mechanical structure, yarn path, insertion system, chopping unit, control system and line interfaces. This systems-based approach is important for equipment that must operate continuously while maintaining fabric uniformity.
The company also maintains an experienced research and development team composed of senior industry engineers. Their work covers structural redesign, functional-module integration, difficult-material processing and non-standard equipment configuration. Such expertise is particularly relevant to the YRS3-M-F-II because the final machine configuration depends strongly on the customer’s material construction.
Stage-by-Stage Production Control
Production begins with the review of the technical specification. This stage confirms the intended fibers, yarn count, package format, working width, target fabric weight, directional ratio, chopped-layer requirement and daily output objective.
Mechanical components are then procured or manufactured according to the approved design. Critical parts require dimensional control because small deviations in alignment, bearing seats, guide positions or insertion elements can influence machine stability and textile quality.
Machining and component preparation are followed by structured assembly. During assembly, the machine frame, drive systems, knitting elements, yarn guides, weft insertion components, chopping equipment and auxiliary systems are brought together according to the approved layout.
Functional testing follows mechanical assembly. Engineers check movement, synchronization, tension paths, safety functions, control responses and operating clearances. The chopping unit and weft insertion system receive particular attention because they directly affect the uniformity and stability of the finished fabric.
Before dispatch, the complete machine is tested and debugged. Where possible, production parameters are reviewed using the customer’s target construction. This allows potential interface or process issues to be identified before installation at the customer’s plant.
Research and Development for Customized Solutions
Composite textile production often involves materials and structures that are not covered by a standard catalogue configuration. Fiber tex, package shape, resin requirements, fabric weight and downstream forming methods can all influence the required machine design.
Yuanyang’s research and development capability supports modifications to the machine structure, functional module integration and process-oriented optimization. This may involve adapting the yarn path, adding a material feed, adjusting the chopping arrangement or revising the line interface.
Customization is not limited to physical hardware. The operating sequence, speed profile, tension settings and control signals may also need to be coordinated with upstream creels, substrate feeders, inspection systems, roll winders or downstream cutting equipment.
Configuration Process for a New Project
Every YRS3-M-F-II project should begin with a clear description of the intended fabric. A sample, drawing, laminate schedule or written construction specification can be used as the starting point. The more complete the technical input, the more accurately the machine can be configured.
The first item to confirm is the fabric’s target areal weight and construction. This determines the likely yarn density, chopped-layer contribution, operating speed and production window. A heavy fabric may require slower operation or a different binding arrangement than a lighter fabric.
The fiber type and yarn specifications must also be defined. Glass fiber and polyester behave differently during tensioning, insertion, chopping and knitting. Yarn tex, filament structure, package format and surface treatment can influence guide selection, tension control and wear behavior.
The required working width and edge trim are reviewed against the nominal 103-inch working width. The usable fabric width may depend on edge formation, downstream cutting requirements and the actual construction. Confirming this information early helps prevent mismatch between the textile line and later processing equipment.
The customer must also specify whether the chopped layer is required, its target weight and its position within the fabric. If a nonwoven material is to be used, its basis weight, width, roll format and handling properties should be provided for technical review.
Daily output targets are evaluated together with the fabric construction. A reference output of 3000 kg per day is available, but actual production depends on the number of machine revolutions, fabric weight, process stability, yarn supply and operating schedule.
Finally, the workshop layout and utilities are reviewed. Floor area, machine orientation, service access, electrical supply, compressed air, material storage, ventilation and roll-handling requirements can all affect installation planning.
| Project Input | Reason for Confirmation | Effect on Configuration |
|---|---|---|
| Fabric construction | Defines the required reinforcement architecture | Influences guides, insertion density and knitting settings |
| Target areal weight | Establishes the material quantity per unit area | Affects yarn density, speed and output |
| Fiber and yarn data | Confirms material behavior and package requirements | Influences creel, tension and wear components |
| 0°/90° ratio | Determines directional reinforcement balance | Sets the relative yarn contribution in both directions |
| Chopped-layer weight | Defines the additional fiber content | Determines chopping-unit and feed settings |
| Nonwoven requirement | Identifies the need for a substrate or carrier layer | May require an additional feed module |
| Workshop layout | Ensures safe installation and service access | Controls line arrangement and utility planning |
| Downstream equipment | Ensures compatibility with winding, cutting or laminating | Defines control signals and roll-handling interfaces |
Installation, Commissioning and Training
Installation is an important part of the machine supply process. A high-performance textile machine must be leveled, aligned, connected and adjusted correctly before it can deliver stable fabric quality.
Yuanyang engineers can attend the customer’s facility for installation and commissioning. They review the machine position, utility connections, yarn paths, material feeds, safety systems and line interfaces. After the mechanical and electrical checks are completed, the machine is operated progressively until the agreed production conditions are reached.
Commissioning focuses on both machine operation and fabric performance. Engineers may review areal weight, directional ratio, chopped-layer uniformity, fabric appearance, edge quality, roll formation and running stability. Acceptance should be based on the agreed fabric specification rather than speed alone.
Operator training can cover machine start-up, threading, yarn-path inspection, tension adjustment, speed changes, chopping-unit operation, routine cleaning and basic fault identification. Maintenance personnel can receive additional instruction in wear-part replacement, lubrication, alignment checks and preventive maintenance.
The company can also support training for workshop management and quality personnel. A one- to two-month training program may be arranged at the customer’s workshop or at the manufacturer’s fabrication facility, depending on the project requirements.
Maintenance and Long-Term Serviceability
Regular maintenance is essential for equipment that handles abrasive glass fiber and operates with multiple yarn systems. The primary wear points on this machine include the chopping unit, weft insertion elements, yarn guides, tension components and selected knitting parts.
Operators should inspect yarn paths at each shift handover. Damaged guides, excessive lint or fiber accumulation, irregular tension and abnormal noise should be addressed before they influence fabric quality or cause unplanned downtime.
The chopping unit requires particular attention because its performance affects the basis weight and distribution of the chopped layer. Blades, feed components and alignment should be inspected according to the maintenance schedule and the abrasiveness of the processed fiber.
Weft insertion elements should be checked for wear, alignment and synchronization. Any irregularity in the cross-machine yarn system can produce visible lines, density variation or localized weakness in the finished fabric.
Preventive maintenance should also include drive systems, bearings, fasteners, electrical cabinets, sensors, safety devices and control interfaces. A planned maintenance schedule is generally more effective than waiting for a component failure, especially in continuous industrial production.
Yuanyang supports spare-parts supply and after-sales assistance through its service network. Long-term technical support can help production teams identify the source of fabric defects, optimize process settings and maintain stable operation after handover.
Quality Control in Fabric Production
Fabric quality is influenced by the relationship between yarn tension, insertion density, stitch formation, chopped-fiber distribution and machine speed. The equipment should therefore be evaluated using the complete fabric construction rather than a single machine parameter.
Areal weight is one of the basic quality indicators. Samples can be weighed at defined positions across the width and along the production direction to identify variation. Results should be compared with the agreed target and tolerance.
The 0°/90° directional ratio should also be verified. This can involve separating or analyzing the directional yarn systems, depending on the fabric construction and available laboratory method. Consistent directional balance is important when the fabric is designed for predictable laminate performance.
Chopped-layer uniformity should be checked by observing coverage, distribution and local accumulation. Excessive variation can affect resin uptake, surface appearance and the mechanical consistency of the composite part.
Roll formation is another important consideration. Tension changes, edge instability or uneven winding can make the fabric difficult to unwind and process. A stable roll structure contributes to efficient storage, transportation and downstream lamination.
Yuanyang applies stage-by-stage inspection to component procurement, machining, assembly, testing and debugging. Every machine is tested before dispatch, providing a controlled basis for installation and acceptance at the customer’s site.
Operational Benefits for Composite Textile Producers
The YRS3-M-F-II can support product diversification. A producer that already manufactures standard biaxial fabrics may use the platform to enter chopped-fiber composite fabrics, hybrid reinforcement products or nonwoven-backed structures.
Its adjustable directional ratio also allows a single production platform to serve several customers or laminate designs. Instead of being limited to one balanced fabric, the manufacturer can develop products with different reinforcement balances and areal weights.
The integrated material concept may reduce the number of separate textile rolls required by a composite processor. Where the application permits, a combined fabric can replace the handling of individual biaxial, chopped-mat and carrier layers.
The machine’s broad 103-inch format is suitable for industrial-width products. Wide production can reduce the number of joints or overlaps required in large composite structures, although the final benefit depends on the component geometry and cutting plan.
The reference output of up to 3000 kg per day provides a basis for high-volume planning. Production managers should calculate actual capacity using the intended fabric weight, operating speed, shift pattern, changeover time, material availability and expected efficiency.
Frequently Asked Questions
What type of machine is the YRS3-M-F-II?
It is a Raschel chopped fiber biaxial warp knitting machine. It combines 0°/90° weft insertion with an integrated chopping unit and a warp knitting structure that binds the reinforcement materials into a stable fabric.
Which fibers can be processed?
The standard applicable fibers are glass fiber and polyester. Other materials may be reviewed for special projects, but suitability must be confirmed according to fiber properties, yarn format, tension behavior and chopping requirements.
Can the 0°/90° weight ratio be customized?
Yes. The weight ratio between the 0° and 90° reinforcement directions can be configured according to the target laminate properties and fabric specification. The final ratio is confirmed during technical design and commissioning.
What is the available chopped-layer weight?
The optional chopped layer is generally configured from 50 to 500 g/m². The appropriate value depends on the required fabric weight, surface coverage, resin-flow behavior and role of the chopped fiber in the final composite.
Can a nonwoven layer be used?
Yes. A suitable nonwoven fabric can be introduced beneath the yarns, either as an alternative to the chopped layer or as part of a combined structure. The nonwoven specification must be reviewed before the feed system is finalized.
What is the typical finished fabric weight?
The greige fabric weight typically ranges from 300 to 2000 g/m². The actual achievable range depends on yarn density, directional ratio, stitch pattern, chopped-layer content and operating conditions.
What is the machine’s working width?
The stated working width is 103 inches for the 0°/90° construction. Final usable width and edge trim should be confirmed according to the customer’s fabric drawing and downstream cutting requirements.
What output can be expected?
The reference daily output is 3000 kg. Actual production varies according to fabric construction, areal weight, speed, yarn supply, process stability, changeover requirements and operating schedule.
Is the machine suitable for wind-power fabrics?
Yes. The machine is positioned for wind-power reinforcement products and nacelle-cover fabrics. Its directional structure, configurable weight ratio and optional chopped or nonwoven layer are useful for composite components requiring broad, stable reinforcement textiles.
How does the HS version differ from the HX version?
Both belong to the chopped-fiber biaxial warp knitting equipment family and can be configured for chopped mats and composite fabrics. The HS configuration is positioned for applications such as wind power and nacelle covers, while the HX configuration serves the same general product family in a different machine configuration. The correct selection should be based on the required fabric, production target and technical layout.
Does the supplier provide installation and training?
Yes. Engineers can support installation, commissioning and operator training at the customer’s plant. Training may cover machine operation, maintenance, fabric inspection, quality documentation and workshop management procedures.
Can the machine be customized?
Yes. Customization may include structure redesign, functional-module integration, material-feed changes, control interfaces, line layout and process optimization. The customer should provide the target fabric, fiber data, workshop plan and downstream process information for evaluation.
Conclusion
The YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine provides a flexible route to producing advanced fiberglass textile constructions. Its combination of 0°/90° directional reinforcement, integrated chopping, optional nonwoven feeding and configurable fabric weight gives it a broader application range than equipment limited to either conventional biaxial fabrics or random chopped mats.
The machine is particularly suitable for composite textile producers serving wind power, nacelle covers and other industrial reinforcement markets. Its 103-inch working width, 50–1000 r/min speed range and reference output of up to 3000 kg per day provide a foundation for large-scale production, while the final performance is tailored to the selected fabric construction.
The strengths of the equipment are supported by Changzhou Yuanyang Electromechanical Technology Co., Ltd.’s manufacturing facilities, engineering experience and customization capability. Stage-by-stage quality control, in-house assembly and testing, research and development support, installation assistance and long-term service all contribute to a complete equipment solution rather than a standalone machine purchase.
For a successful project, the customer should define the required fabric architecture, fiber and yarn specifications, directional ratio, chopped-layer weight, nonwoven requirement, output target and workshop conditions at an early stage. With these inputs, the YRS3-M-F-II can be configured as a production platform that supports repeatable, scalable and application-specific composite textile manufacturing.
References
1. Changzhou Yuanyang Electromechanical Technology Co., Ltd., Technical Information for the YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine.
2. Changzhou Yuanyang Electromechanical Technology Co., Ltd., Product Information for Fiberglass Textile Machinery and Biaxial Warp Knitting Equipment.
3. Composite Materials Handbook, General Principles of Reinforcement Architecture and Textile Preforms.
4. Industrial Textile Engineering References, Warp Knitting, Weft Insertion and Stitch-Bonded Fabric Construction.
5. Technical Guidance on Glass-Fiber Reinforced Polymer Fabrication and Composite Laminate Processing.
Product: YRS3-M-F-II Raschel Chopped Fiber Biaxial Warp Knitting Machine(HS)
News
-
Three quotations land on the same desk for the same polyester nonwoven line, and on paper they look interchangeable. Each is priced per metre of working width. Each quotes a similar top speed. Each c...
READ MORE -
Two quotations land on the same desk. Both offer a multiaxial warp knitting line, both list the same working width, both promise high output. One buyer signs and discovers six months later that the f...
READ MORE -
Match the machine type to the fabric: choose a tricot Warp Knitting Machine for fine, smooth fabrics such as lining and sportswear, a raschel machine for open, patterned, and technical fabrics, a doub...
READ MORE -
Two buyers open the same catalogue and both ask for a warp knitting machine. One needs a 4.5 m wide glass-fibre geogrid with 0° and 90° yarns stitched together for a soil-reinforcement contract; the ...
READ MORE
-
Contact Info.
+86-198 5534 1617
+86-134 0158 3002yuanyang@yywarpknitting.com 699#, Shengzhi West Rd, Lvcheng Town, Danyang City, Zhenjiang City, Jiangsu Province, China

-
QR Code
-
Quick Links
Home About Products Manufacturing Customization News Contact -
Product List
Machine for Chemical Fiber Textile Machine for Fiberglass Textile Machine for Carbon Fiber Textile -
About Us
Company Profile Factory Gallery Value-added Service
Copyright © 2026 Changzhou Yuanyang Electromechanical Technology Co., Ltd. All Rights Reserved.
Custom Warp Knitting Machine Manufacturers
